Square bottom FIBCs are becoming practical tools for cleaner, faster, and more stable bulk handling. Their four-panel construction helps bags stand upright during filling, storage, and transport. This matters when warehouses face narrow aisles, uneven pallets, or repeated loading schedules. Grand View Research identifies flexible intermediate bulk containers as a growing global packaging segment, supported by chemicals, food ingredients, agriculture, and construction materials. MarketsandMarkets also links demand growth with lightweight transport packaging and improved warehouse efficiency.
A reliable supplier must offer more than attractive product photos. The China Leading Square Bottom Fibc Supplier should explain fabric weight, safe working load, safety factor, liner options, lifting loops, discharge designs, and seam quality. Experienced manufacturers normally verify dimensions and load performance through controlled inspections. ISO 21898 provides a useful reference for FIBC construction and testing. Independent laboratory reports can further support claims about strength, cleanliness, and application suitability. Food-grade projects may also require specific material declarations and traceability records.
Small details matter. A stiff corner seam can affect stacking. A poorly fitted liner can slow discharge. These problems are easy to overlook. No supplier is perfect, and specifications still need practical review before mass production. Buyers should request samples, inspect filled bags, and compare pallet stability under real handling conditions. This introduction examines how a China Top Square Bottom FIBC Bag Supplier can combine manufacturing experience, documented quality systems, and responsive technical support. The goal is not merely lower packaging cost. It is safer handling, better cubic utilization, and dependable performance from the factory floor to the final warehouse.
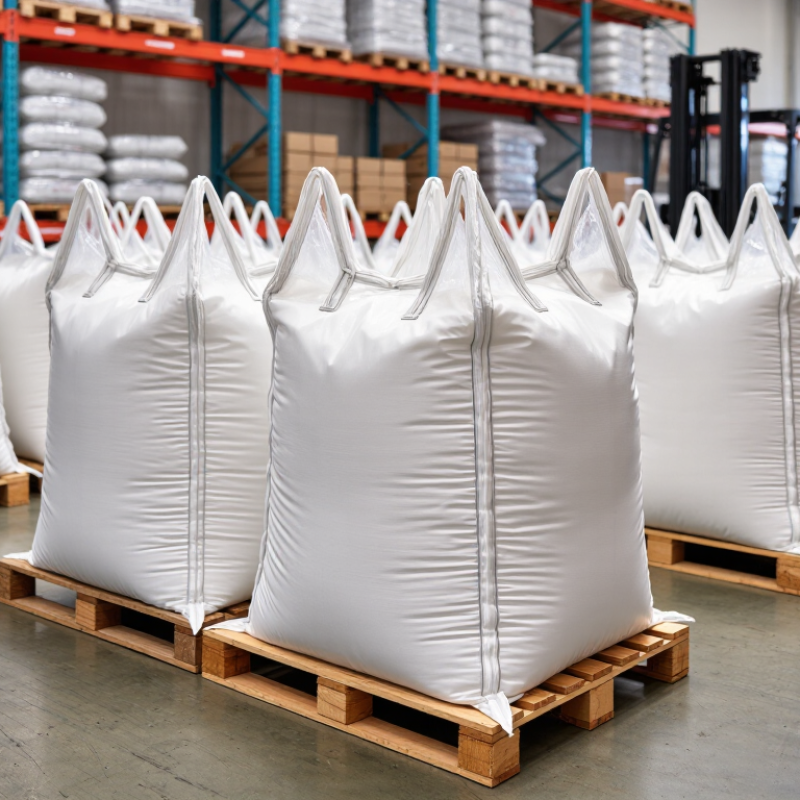
Square bottom FIBC bags support stable stacking for powders, granules, and agricultural materials. Their four-panel base reduces tipping during storage and transport. Common designs carry a safe working load from 500 to 2,000 kg.
The 5:1 safety factor means a 1,000 kg bag should withstand a 5,000 kg minimum break load under defined test conditions. This does not permit overfilling. ISO 21898:2004 outlines performance requirements for flexible intermediate bulk containers, including lifting, testing, and labeling controls. Industry handling guidance also stresses balanced filling and vertical lifting loops.
Details matter. A 2,000 kg bag needs stronger fabric, reinforced seams, and carefully designed corner construction. The bottom must remain square after filling. Otherwise, stacking stability can decline. Drop tests, cyclic lifting tests, and seam inspections provide useful evidence before shipment. Still, laboratory results cannot reproduce every warehouse floor, forklift movement, or humid storage area. That is where specifications sometimes need review. Proper loading, dry storage, and routine inspection remain essential. A reliable supplier should provide test records, material information, and clear working-load instructions for each design.
Durable bulk bags begin with controlled raw materials, not attractive stitching alone. We typically select woven polypropylene tapes with stable melt flow and consistent denier. These details influence tensile strength, elongation, and fabric uniformity. Virgin polypropylene often provides dependable performance for demanding applications. Recycled content may reduce material use, but its quality must be verified carefully. It is not automatically equal.
Fabric construction matters. Tapes should remain evenly spaced, with no visible gaps or weak edges. Lamination can improve moisture resistance, yet excessive coating may reduce flexibility. Square bottom panels need accurate cutting and balanced sewing tension. Otherwise, the filled bag may lean or bulge under load. Small differences become obvious during handling.
Testing should reflect real warehouse conditions. We check fabric tensile strength, seam strength, lifting loops, drop resistance, and safe working load. Samples should also face visual inspection before shipment. A clean surface is useful evidence, but it proves little by itself. Records of batch numbers, test results, and inspection dates support traceability.
In practice, one overlooked seam can affect an otherwise well-made FIBC. That is where we still need to improve. Supplier communication also matters, especially when customers change filling density, storage time, or transport conditions. Proper woven polypropylene standards must match the actual application, not just a specification sheet.
China Top Square Bottom FIBC Bag Supplier
Manufacturing starts with fabric cutting. Polypropylene woven rolls are measured, aligned, and cut into panels for stable dimensions. Small errors can distort the square bottom. We still see this when fabric tension changes during production. That detail deserves more attention.
Sewing follows a controlled pattern. Reinforced corners, lifting loops, and discharge spouts must match the approved drawing. Operators check stitch density and seam width by sampling each production batch. ISO 21898 provides requirements for flexible intermediate bulk containers, including construction and performance testing. A safe design often uses a 5:1 safety factor, meaning the tested load is five times the rated working load. It is not a substitute for correct filling and handling.
Coating adds resistance against moisture, dust, and fine powders. The coating must cover evenly without blocking the fabric’s flexibility. Inspectors examine pinholes, weak edges, and uneven gloss under direct light. Load testing then places filled bags under lifting, stacking, and repeated handling conditions. Test records should identify the bag type, working load, test load, duration, and failure point. According to packaging industry market assessments published in 2024, demand continues to favor higher-strength bulk packaging and more consistent quality control. Yet laboratory results can differ from warehouse reality. Humidity, sharp pallets, and rushed lifting still create unexpected failures. A reliable Chinese supplier should review these conditions before approving final production.
| Manufacturing Stage | Typical Data or Dimension | Process Description | Quality Control Method | Reference Requirement or Acceptance Criteria |
|---|---|---|---|---|
| Raw Material Preparation | Virgin or approved recycled polypropylene (PP); fabric basis weight commonly 140–220 g/m² | PP resin is converted into tapes, which are woven into tubular or flat fabric for the body, panels, base, and top sections. | Check resin documentation, fabric appearance, basis weight, tape width, and weave consistency. | Material selection must match the required safe working load, filling method, discharge design, and product-contact requirements. |
| Fabric Cutting | Typical finished bag size: 90 × 90 × 110 cm; dimensional tolerance commonly controlled within ±2% | Woven fabric is cut into accurately sized body panels, square-bottom panels, top panels, discharge tubes, and lifting-loop components. | Use calibrated cutting templates or CNC cutting equipment; measure panel length, width, squareness, and seam allowance. | Cut edges should be straight, free from excessive fraying, and consistent with the approved technical drawing. |
| Fabric Coating | PP coating commonly adds approximately 15–40 g/m², depending on leakage and moisture-barrier requirements | A polypropylene coating is applied to one side of the woven fabric to improve fine-powder retention, moisture resistance, and surface stability. | Inspect coating coverage, adhesion, pinholes, wrinkles, surface uniformity, and coating weight. | The coating should be continuous in the specified area and must not interfere with folding, sewing, filling, or discharge operations. |
| Panel Sewing | Common seam construction: double-chain or lock stitching; seam allowance typically 25–40 mm | Body panels are joined to create the square-shaped container, with reinforced seams at the corners and stress-bearing areas. | Check stitch density, skipped stitches, thread tension, seam alignment, and visible needle damage. | Seams must be continuous, secure, and free from open sections, loose thread ends, skipped stitches, or fabric tearing. |
| Square Bottom Assembly | Typical base panel: approximately 90 × 90 cm for a 90 × 90 cm bag body | The bottom panel is sewn to the four body sides to form a stable square base suitable for palletized storage and transport. | Verify base squareness, corner matching, seam overlap, flatness, and absence of gaps along the bottom seam. | The finished base should sit evenly on a flat surface without abnormal leaning, twisting, or unsupported corners. |
| Lifting Loop Installation | Four-loop construction is common; loop width often ranges from 50–70 mm | Webbing or integrated lifting loops are positioned at the four corners and sewn into reinforced load-bearing areas. | Check loop position, length, webbing condition, stitch pattern, and reinforcement patch dimensions. | All loops must be aligned and capable of transferring the rated load to the body without visible deformation or seam separation. |
| Top and Discharge Components | Common options: open top, duffle top, filling spout, flat bottom, or discharge spout | The selected filling and discharge arrangements are sewn to the top and bottom according to the handling and material-flow requirements. | Inspect tube diameter, length, drawcord operation, tie closure, seam security, and compatibility with filling equipment. | Closures should operate smoothly and maintain the required containment performance during handling and transportation. |
| Cleaning and Visual Inspection | 100% visual inspection of finished bags | Loose threads, fabric debris, oil marks, contamination, and packaging defects are removed before final testing and packing. | Inspect body, seams, loops, coating, labels, closures, dimensions, and overall appearance against the approved sample. | No holes, critical contamination, broken load-bearing stitches, incorrect components, or unidentified product deviations are accepted. |
| Safe Working Load Verification | Typical commercial rating: 500–2,000 kg; example reference rating: 1,000 kg | The rated capacity is established from the fabric, seam, loop, base, filling, and discharge designs rather than from bag volume alone. | Review design calculations, component specifications, production records, and representative test results. | The declared safe working load must be clearly identified and must not be exceeded during use. |
| Load Testing | Example test load: 1,000 kg rated load; safety factor selected according to the intended bag type | A filled bag is lifted and assessed for deformation, seam damage, loop failure, bottom failure, and load retention. | Conduct representative top-lift, bottom-lift, compression, drop, or cyclic tests when required by the specification. | Testing and acceptance should follow the applicable design specification and ISO 21898 requirements for flexible intermediate bulk containers. |
| Final Measurement and Packing | Finished dimensions recorded in centimetres; bundles commonly compressed and wrapped for shipment | Approved bags are folded, counted, bundled, protected from moisture, and prepared for container loading or pallet shipment. | Verify quantity, bag identification, dimensions, packaging integrity, and traceability records. | Packaging must prevent contamination and moisture damage while preserving clear identification of size, construction, and rated capacity. |
China Top Square Bottom FIBC Bag Supplier
For square bottom FIBC bags, quality control begins with ISO 21898 requirements for non-dangerous goods. Our inspection process checks fabric weight, seam strength, dimensions, lifting loops, and discharge spouts. Each production batch receives a documented identification code. Traceability matters.
A laboratory test measures safe working load and safety factor before shipment. Drop testing also examines whether filled bags keep their shape after impact. The square base should stand evenly on a pallet, without twisted corners or loose stitching. Inspectors record visual defects, contamination risks, and moisture exposure.
UNCTAD’s Review of Maritime Transport 2023 states that about 80% of global merchandise trade by volume moves by sea. Long transit can expose packaging to vibration, stacking pressure, and changing humidity. Therefore, inspection cannot stop at the sewing line. Sample retention and container-loading photos provide useful evidence.
Still, no inspection system is perfect. A rushed visual check may miss internal fabric damage. We review failed samples and adjust operator training. This step is less impressive, but often more valuable. Batch records connect raw fabric, sewing dates, test results, and shipment details, supporting reliable investigation when an issue appears. Supplier audits should also verify calibrated equipment, trained inspectors, and complete corrective-action records.
China Top Square Bottom FIBC Bag Supplier
Customization Options for Food, Chemical, and Construction Material Packaging
A reliable square bottom FIBC bag begins with the product, not a standard catalog size. Our packaging experience shows that filling behavior, storage height, and discharge speed must guide each design. Food applications may require clean polypropylene fabric, food-contact liners, dust-resistant seams, and dedicated production controls. Transparent inspection windows can also help operators check material levels without opening the bag.
Chemical powders and granules often need coated fabric, antistatic features, stronger lifting loops, or an inner liner. These choices depend on the material’s flow, moisture sensitivity, and handling conditions. Compatibility testing remains essential. A bag may look suitable and still perform poorly with a different chemical powder. That detail is easy to miss.
Construction materials demand practical strength. We can adjust fabric weight, top openings, bottom discharge spouts, dimensions, and UV resistance for outdoor storage. A square shape improves pallet stability and uses warehouse space efficiently. Printing can identify batch details, handling instructions, or filling limits. Clear markings reduce mistakes on busy sites.
Small details matter. Yet customization should not become unnecessary complexity. Every option should support safer filling, transport, or unloading. Some designs need revision after a trial run, especially when material flow changes with humidity. Careful sampling, seam inspection, and load testing help confirm performance before regular production. Specifications should always match applicable packaging and transport requirements in the destination market.
Common safe working load ranges for square-bottom FIBC bags vary by fabric strength, lifting construction, liner selection, filling method, and handling conditions. The chart shows commonly specified planning ranges; the final load rating must be confirmed through product testing and applicable packaging requirements.
Food packaging commonly uses hygienic polypropylene fabric and optional food-contact liners. Chemical packaging may require sift-proof seams, antistatic construction, or UN performance certification. Construction-material packaging typically prioritizes higher load capacity, abrasion resistance, and discharge options. Reference framework: ISO 21898 for flexible intermediate bulk containers.
Whether you’re a homeowner, builder, or designer, you’ll find that our elegant cabinets create a breathtaking space that evokes positive emotions and encourages lasting memories. We invite you to explore our website to learn more about who we are and how we can help you.
Woodinville | Bellevue | Seattle | Kirkland | California | Berkeley | Walnut Creek | Roseville, CA
© 2025 Acadia Craft. Powered by Integrity Marketing Serving Woodinville, Kirkland, Bellevue & The Greater Seattle Area
